When a stepped hole needs one pass
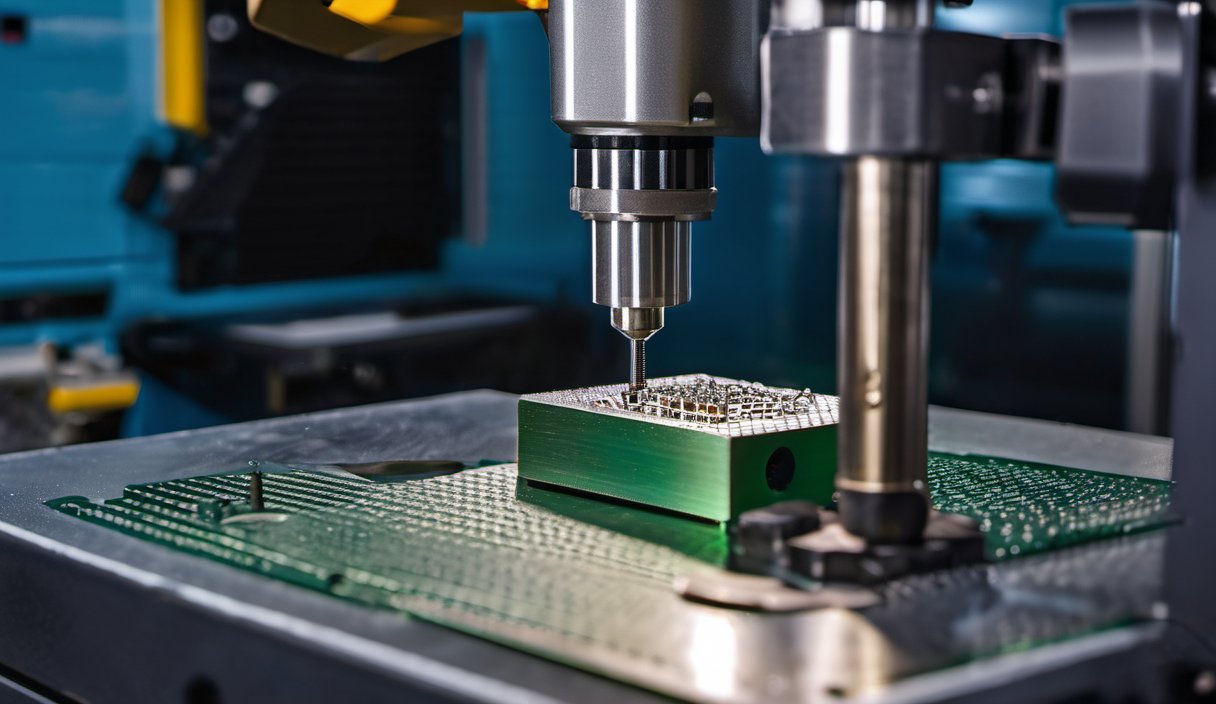
A stepped hole normally means two tools, two tool changes and a concentricity risk between them. A step drill grinds both diameters into one body, which is why our largest series is not a standard drill at all.
The scale of the series
HDCS636 has 1,508 distinct part numbers. It is a TiN-coated left-hand step drill family, and almost every entry is a non-standard geometry written for a specific board or component stack.
A typical record looks like this:
D1.45*3.7*120°+1.85*4.0*70°*3*38
Read it as two cutting stages joined by a +: a 1.45 mm stage with a 120° point, then a 1.85 mm stage with a 70° point, on a 3 mm shank and 38 mm overall length.
Why the string is kept verbatim
It is tempting to store only the first diameter. That would make the catalogue easier to sort and useless to an engineer. We keep the full string on the part-number page and mark it as non-standard geometry, with a note to request the dimensioned drawing before ordering.
| Field | What it controls |
|---|---|
| Stage diameters | Hole and counterbore size |
| Stage lengths | Depth of each step |
| Point angles | Entry behaviour and exit burr |
| Shank / overall | Holder and reach |
Before you design a new one
Search the record by diameter and by series first. With 1,508 existing variants, the geometry you need is often one suffix away from a tool that has already been ground.
Send the two diameters, the two depths and the shank. We check the production record before proposing a new grinding programme.